2026 Top Sanitary Napkin Making Machines Buying Guide
Choosing a Sanitary Napkin Making Machine in 2026 requires more than comparing speed, price, and polished brochures. The right decision begins with production reality: local absorbent materials, available floor space, trained operators, power stability, and expected daily output. A compact workshop may need a dependable semi-automatic line. A large manufacturer may require servo control, automatic stacking, multi-size conversion, and documented quality checks.
Arunachalam Muruganantham, a renowned social entrepreneur and sanitary-pad machine innovator, has said, “The real problem is not making sanitary pads, but making them affordable.” That principle remains important. A fast machine is not automatically a wise investment. Its maintenance cost, spare-part access, energy use, and reject rate can quietly shape profitability.
This 2026 Top Sanitary Napkin Making Machines Buying Guide examines those practical details. It considers forming systems, sealing accuracy, packaging options, operator safety, and after-sales support. Look closely at the pad edge. Inspect the core alignment. Ask how quickly a technician can respond.
Some specifications look impressive.
They may not fit your factory.
Buyers should also question optimistic capacity claims. Real output can fall when materials change, workers need training, or small faults interrupt production. A reliable supplier should provide testing records, clear warranty terms, installation guidance, and sample products made with your materials. No machine removes every production problem. Careful selection reduces avoidable ones.
This guide aims to support evidence-based purchasing, while recognizing an uncomfortable truth: the cheapest quotation can become the most expensive decision.
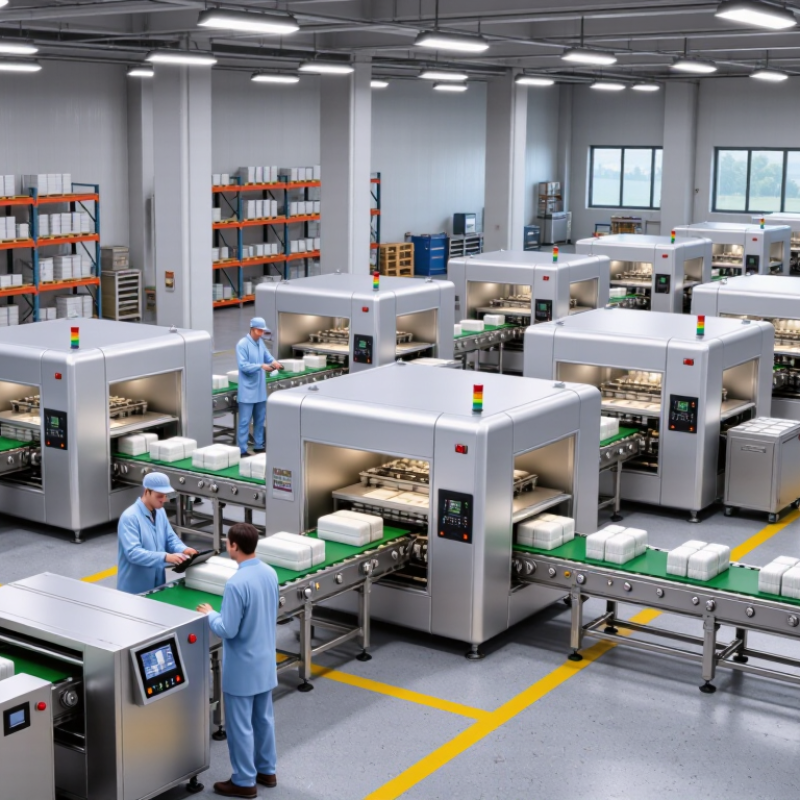
Sanitary Napkin Machine Types and 2026 Production Speeds of 600–1,200 Pieces/Minute
In 2026, sanitary napkin machinery is moving toward rated speeds of 600–1,200 pieces per minute. At 600 pieces, a line theoretically produces 36,000 pieces hourly. At 1,200, that figure reaches 72,000. Real output is lower. Changeovers, material splices, rejects, and maintenance reduce performance. Field planning should use an 80–90% efficiency assumption, not the headline speed.
According to Smithers’ technical outlook on hygiene products, manufacturers increasingly prioritize thinner structures, improved fluid distribution, and lower material waste. These requirements affect machine selection. A high-speed line must control pulp forming, absorbent-core placement, release paper cutting, sealing, folding, and individual wrapping without damaging the product. Industry market studies from Grand View Research also indicate continued growth in feminine hygiene demand, supporting investment in automated, flexible equipment. Still, market growth does not guarantee quick payback.
Buyers should inspect hourly good output beside the machine, with samples running. Ask for speed data using the intended core weight, pad length, and packaging format. Servo-controlled systems usually support faster adjustments, but they can require stronger technical skills. Energy use, compressed-air demand, spare-part availability, and operator training deserve equal attention. A spreadsheet can make this look simpler than it is. The advertised 1,200 pieces per minute may only apply to one narrow product specification. Acceptance testing should measure sustained output, reject rate, changeover time, and safety performance under normal factory conditions.
2026 Top Sanitary Napkin Making Machines Buying Guide
Typical production-speed ranges for major sanitary napkin machine types
Modern high-speed sanitary napkin production lines commonly operate between 600 and 1,200 pieces per minute. Actual output depends on product dimensions, absorbent-core structure, raw-material quality, packaging configuration, changeover frequency, and machine automation level. The ranges shown are practical planning benchmarks rather than guaranteed output for every production line.
Key Machine Specifications: 160–330 mm Product Width and 100–300 GSM Core Weight
2026 Top Sanitary Napkin Making Machines Buying Guide
Machine specifications deserve more attention than headline production speed. A practical starting range is 160–330 mm for finished product width. This range supports slim, regular, and larger sanitary napkin formats. According to Grand View Research, the global feminine hygiene products market was valued at approximately USD 42.7 billion in 2022. Its projected growth increases pressure on manufacturers to improve flexibility and consistency.
Core weight is equally important. A 100–300 GSM range allows manufacturers to adjust absorbency, softness, and material cost. Lower GSM cores may suit light-flow products, while higher GSM structures can support heavier absorbency requirements. However, more material does not automatically mean better performance. That assumption needs testing. EDANA’s absorbency and liquid-retention test methods are useful references during product validation. Operators should compare core weight with acquisition speed, leakage resistance, and compression recovery.
Width and GSM settings must work together. A 330 mm product with a 100 GSM core may feel poorly balanced. A narrow product with 300 GSM may become unnecessarily bulky. Machine buyers should inspect servo control, forming accuracy, tension stability, and GSM deviation across the web. Small errors compound. In factory trials, measure at least ten samples from different production moments. Record width, thickness, weight, and absorbency. The process may look stable, but early data can be misleading.
2026 Top Sanitary Napkin Making Machines Buying Guide - Key Machine Specifications: 160–330 mm Product Width and 100–300 GSM Core Weight
Automation, Servo Control, and OEE Benchmarks Above 85% for Modern Lines
Buying a sanitary napkin line in 2026 means buying stable output, not merely higher speed. In factory audits, strong lines combine servo-driven forming, tension control, and automatic web correction. They keep absorbent cores centered while belts change speed. Small deviations matter. A two-millimeter shift can create edge exposure, rejects, and uncomfortable products.
OEE should guide the purchase, but it must be measured honestly. The OEE Foundation identifies 85% as a world-class reference, calculated from availability, performance, and quality. That figure is demanding. During acceptance testing, request separate losses for film breaks, changeovers, micro-stops, and quality holds. A dashboard showing 92% OEE means little without clear downtime definitions. The 2024 PMMI State of the Industry reporting also highlights growing demand for connected controls and production visibility in packaging plants.
Servo systems support accurate registration and recipe changes for different pad sizes. Test at least three products, two material lots, and one realistic changeover. Record good pieces per minute, waste percentage, and recovery time. Do not trust the dashboard alone. Operators still influence OEE through cleaning discipline, training, and fault response. That human factor is easy to underprice. An 85% target may also hide weak quality checks, so buyers should verify laboratory results and retained samples before approving the line.
Machine Costs, Energy Use, Compliance, and Payback Within 2–4 Years
A 2026 sanitary napkin machine purchase should begin with total ownership cost, not the catalogue price. Industry quotations commonly place semi-automatic lines near USD 100,000–300,000, while high-speed integrated systems may exceed USD 1 million. Installation, tooling, freight, spare parts, and operator training can add 15–30%. These figures are planning ranges, not guarantees.
Energy deserves closer measurement. The International Energy Agency reported only 2.2% global energy-intensity improvement in 2022, showing why efficiency cannot be assumed. Request measured electricity use per 1,000 pieces, not only motor ratings. A line using 0.08 kWh per 1,000 pieces can still waste money through idle heaters, compressed-air leaks, or poor changeover control. Install sub-meters. Compare real production data after 30 days.
Compliance affects both cost and payback. Test absorbency, leakage, skin-contact safety, packaging claims, and chemical restrictions under the destination market’s requirements. ISO 9001 supports traceability, while ISO 50001 provides a structured energy-management framework. The WHO and UNICEF Joint Monitoring Programme also highlights menstrual health’s connection with safe, acceptable products and services. A realistic payback model should include yield loss and rejected packs. At USD 0.01 saved per pad, producing 25 million pads monthly creates USD 250,000 in annual savings. That may support a two-to-four-year payback, but only with stable orders. I would not promise it without verified uptime, scrap records, utility tariffs, and local compliance costs.


