China Top Hospital Supplies Manufacturers for Global Buyers
China has become a major sourcing destination for hospital supplies, serving hospitals, distributors, and healthcare projects worldwide. Its manufacturing base covers examination gloves, surgical instruments, hospital beds, patient monitors, wound-care products, and disposable medical items. Yet product variety alone does not guarantee dependable supply. Global buyers need evidence, not impressive catalogues.
Reliable manufacturers usually combine specialized production lines with documented quality controls. Buyers should examine factory experience, product specifications, material standards, and applicable certifications. Batch numbers should be easy to trace. Packaging should protect sterile products during long-distance transport. A practical review may include sample testing, factory audits, production photos, and clear communication about lead times. These details matter when a carton arrives with damaged seals or unclear labels. Small errors can create large operational problems.
China has many capable producers, but performance differs between factories. Some excel at custom orders, while others focus on stable, high-volume production. Medical equipment suppliers may offer installation support, training, and maintenance guidance. Disposable-product manufacturers may provide stronger capacity and packaging flexibility. Buyers should compare more than prices. After-sales response, replacement policies, documentation, and export experience deserve equal attention.
No supplier is flawless.
A careful selection process remains essential. This guide introduces leading China hospital supplies manufacturers through practical criteria, including manufacturing capability, quality management, product range, compliance awareness, and international service. The goal is not to promote every company equally. It is to help global buyers ask sharper questions, reduce avoidable risks, and build more reliable healthcare supply partnerships. Some information may change over time, so independent verification remains necessary before purchase.
What Defines a Hospital Supplies Manufacturer in China
China Top Hospital Supplies Manufacturers for Global Buyers
What Defines a Hospital Supplies Manufacturer in China
A reliable hospital supplies manufacturer offers more than competitive pricing. It controls design, production, inspection, and shipment preparation. Buyers should examine factory experience with comparable products, not only online catalogs. A professional facility can explain material choices, production tolerances, and product testing clearly. It should also maintain traceable records for raw materials and finished goods. Certifications such as ISO 13485 may support confidence, but certificates require careful verification. A document alone proves little.
Real manufacturing experience appears in small details. Workers follow written procedures and inspect products at defined stages. Samples should match later mass production. Packaging must protect sterile or sensitive items during long transport. Clear technical files, inspection reports, and export documents also show operational maturity. Communication matters. Delayed answers often become delayed shipments. Still, even experienced factories can make mistakes. One inspection method may miss defects, especially when production changes quickly.
Tips: Request samples from the actual production line. Ask for recent audit evidence and batch traceability records. Confirm acceptable defect limits before signing an order. Review packaging with photographs and drop-test information. Discuss corrective action procedures openly. A factory willing to admit weaknesses may be more dependable than one promising perfection. Test communication through a small trial order. Be cautious when every answer sounds effortless.
How China’s Hospital Supply Industry Is Organized
China Top Hospital Supplies Manufacturers for Global Buyers
How China’s Hospital Supply Industry Is Organized
China’s hospital supply industry is organized through regional manufacturing clusters, specialized workshops, and export-focused trading companies. Production is rarely handled by one facility alone. A factory may assemble hospital beds, while nearby suppliers produce frames, motors, wheels, or control systems. This structure helps manufacturers adjust product specifications for different hospitals and purchasing systems.
Medical consumables follow another pattern. Producers often focus on one narrow category, such as protective garments, examination tables, stainless steel carts, or disposable procedure items. Larger facilities may manage molding, packaging, quality inspection, and shipping internally. Smaller factories usually depend on local partners for components and international documentation. The difference matters when buyers assess capacity, traceability, and delivery stability.
From supplier audits, practical verification should include factory licenses, quality records, material information, and production samples. A polished catalog is not enough. Buyers should compare the sample with the final packing list and approved specifications. Communication can also reveal weaknesses. Some suppliers respond quickly but avoid detailed technical questions. Others provide careful answers yet need longer production schedules.
The industry is efficient, but not flawless. Component shortages can delay an otherwise simple order. Translation errors may affect dimensions or packaging labels. I have also seen buyers choose the lowest quotation and later face costly corrections. A stronger process uses clear drawings, staged inspections, and written acceptance criteria before production begins. Reliable cooperation grows from evidence, not confident promises.
Major Product Categories for Global Healthcare Buyers
Global hospital buyers usually begin with product categories, not isolated items. Diagnostic imaging equipment includes ultrasound systems, mobile X-ray units, and patient monitoring devices. These products support fast decisions in emergency rooms and outpatient clinics. Buyers should check image clarity, alarm accuracy, software compatibility, and maintenance access. A low purchase price can become expensive when spare parts are difficult to obtain.
Surgical and critical-care categories require stricter evaluation. Operating tables, anesthesia workstations, infusion pumps, and electrosurgical equipment must match clinical workflows. Infection-control products include sterilizers, washer-disinfectors, medical waste containers, and protective supplies. Stainless-steel surfaces, clear instructions, and validated cleaning processes matter. Small design flaws can slow an entire department.
Laboratory equipment forms another major category for hospitals and diagnostic centers. Common products include hematology analyzers, chemistry analyzers, centrifuges, microscopes, and specimen refrigerators. Buyers should request performance data, calibration procedures, training plans, and service response times. Hospital beds, examination lights, trolleys, and emergency carts also affect daily care. They seem basic. They are not. A crowded ward may reveal weaknesses that a showroom cannot show. Some procurement decisions still rely too heavily on brochures, which is a practical mistake. On-site testing, documented quality systems, and transparent export experience provide stronger evidence of a manufacturer’s reliability.
How to Evaluate Chinese Hospital Supplies Manufacturers
China Top Hospital Supplies Manufacturers for Global Buyers
How to Evaluate Chinese Hospital Supplies Manufacturers
Choosing a Chinese hospital supplies manufacturer requires more than comparing online prices. Start with the product category, intended use, and destination-market requirements. A supplier should explain its quality system clearly. Ask for current certificates, factory licenses, product specifications, and traceability procedures. Check whether documents match the actual production site.
Request samples from the same production line used for bulk orders. Inspect packaging, labeling, dimensions, materials, and visible defects. For sterile products, review sterilization methods, batch records, and packaging integrity tests. Confirm how the manufacturer handles complaints, recalls, and nonconforming products. These details often reveal more than polished sales presentations.
Visit the factory when possible. Observe incoming inspection, clean areas, warehouse conditions, and final packing. Ask to see calibration records and training logs. A video tour helps, but it cannot replace an independent audit. Verify production capacity through purchase records and staffing patterns. Be cautious when one supplier claims expertise across unrelated medical categories.
Communication also matters. The manufacturer should answer technical questions with evidence, not vague promises. Agree on inspection standards, change-notification rules, delivery terms, and document control before placing an order. A quality agreement can prevent expensive misunderstandings. My own evaluation would not rely on a single successful sample; samples can hide process weaknesses. Recheck performance after production begins. Keep written records of every decision.
Key Steps for International Sourcing and Quality Assurance
China Top Hospital Supplies Manufacturers for Global Buyers
International sourcing should begin with a clear product specification, not a low quotation. Define materials, dimensions, packaging, intended use, and required certifications. Request the manufacturer’s registration details, quality management records, and recent inspection reports. Verify certificates with the issuing authority when possible. A factory audit should examine production areas, staff training, equipment maintenance, and complaint handling. Photos are useful, but they are not enough.
Order samples before approving a large shipment. Check fit, labeling, surface condition, sterility claims, and packaging strength. For higher-risk supplies, use an independent laboratory for performance or biocompatibility testing. Confirm lot numbers and traceability from raw materials to finished cartons. Agree on inspection standards before production begins. Include acceptable defect limits, sampling methods, delivery terms, and corrective actions in the purchase contract. One common mistake is trusting a successful sample too quickly. Production consistency still needs proof.
Tips: Keep a document checklist. Compare sample results with technical requirements. Ask for batch records and retention samples. Inspect before shipment, not after problems arrive. Leave time for rework. Communication can fail over small wording differences, so use drawings, photos, and signed specifications. A clean factory does not guarantee every shipment is perfect; continuous verification remains necessary.
China Medical Supplies Sourcing: Quality Assurance Priorities
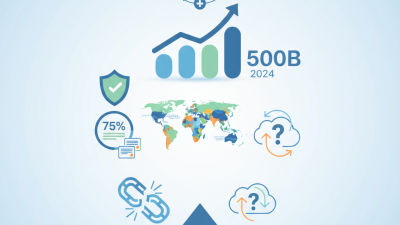
This planning model allocates due-diligence attention across the main international sourcing stages. Regulatory compliance, supplier quality systems, product verification, traceability, inspection and testing, and logistics controls should be assessed before a medical-supply order is approved. The percentages represent a practical quality-assurance allocation framework rather than company or brand performance data.